

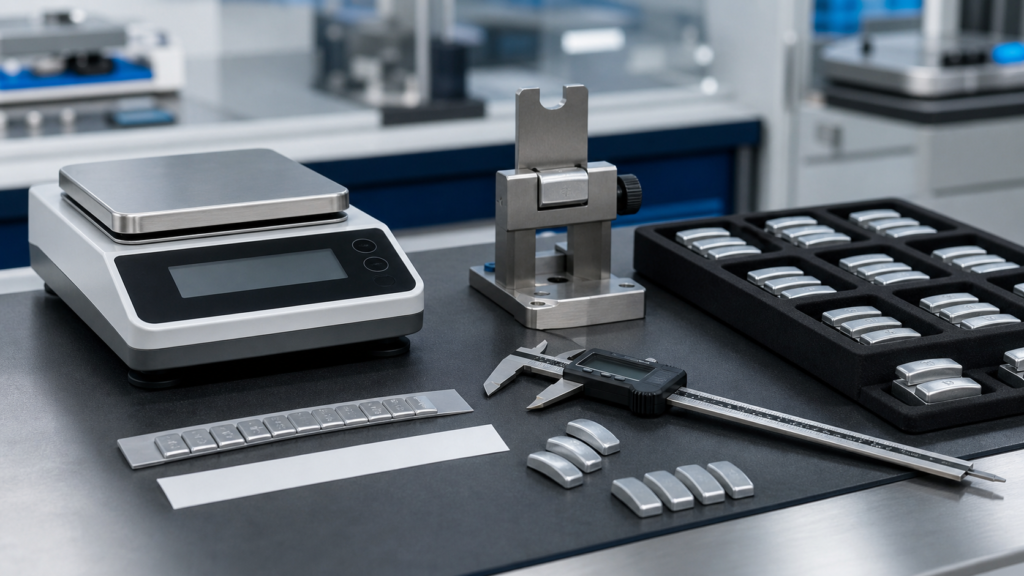
A wheel weight QC checklist should verify the exact SKU and revision, measured mass, dimensions, clip retention or adhesive performance, finish, pack contents, and lot identity. For each check, record the sample, method, agreed limit, actual result, and disposition. Hold goods when identity or acceptance requirements remain unresolved.
Use production and finished-goods QC to compare the current lot with its approved specification. Keep the raw readings and attachment-test conditions with the lot record. If the product has not yet been defined, start with the wheel weight selection framework.
Table of Contents
- What should wheel weight QC control?
- How do sample approval, production QC, and pre-shipment checks fit together?
- How should a buyer write the specification before inspection?
- What does a practical wheel weight QC matrix look like?
- How should weight, markings, and dimensions be checked?
- How should clip retention and adhesive tape be checked?
- What should finish, packaging, and traceability inspection cover?
- What happens when an inspection result fails?
- What evidence should the buyer request before release?
- Conclusion: Make every release decision traceable
- Frequently Asked Questions
- References
What should wheel weight QC control?
Set separate checks for identity, mass, dimensions, attachment, finish, packs, and lot records. Each needs a stated acceptance rule and an observable result.
Start with the product definition rather than the measuring tool. The wheel-balancing weights range contains different attachment methods, materials, profiles, increments, and pack formats. A report has little value if the sample came from a similar-looking SKU or if the approved sample was never assigned a revision.
Clip-on and adhesive weights need separate control lines because their risks are different. Clip-on products depend on the correct rim interface, profile, seating, and retention. Adhesive products depend on tape identity, liner condition, surface preparation, pressure, temperature, dwell, and the intended wheel finish.
Keep the lot header, sample results, and disposition together. The record fields below can be copied into the inspection sheet.
How do sample approval, production QC, and pre-shipment checks fit together?
Sample approval answers whether the proposed product is acceptable; production QC answers whether the current lot still matches it; pre-shipment inspection answers whether the finished shipment can be released. The three decisions should share the same product identity and acceptance rules, but one record should not pretend to replace the others.
| Inspection stage | Main question | Evidence to connect |
|---|---|---|
| Sample approval | Does the representative product, fitment, tape, finish, and pack configuration meet the requirement? | Approved sample, drawing or specification, photos, revision |
| Production QC | Does the current lot match the approved product and defined limits? | Sample IDs, raw readings, test method, defect record |
| Pre-shipment release | Do the cartons, quantities, labels, and documents match the order? | Carton photos, packing list, shipment report, release decision |
Use the separate wheel weight sample approval process to establish the reference product. At the end of production, use the pre-shipment inspection process to reconcile the approved reference with the goods being loaded.
How should a buyer write the specification before inspection?
Define the product, acceptance criteria, and evidence before inspection. An order stating only “wheel weights” leaves the inspector without a usable reference.
| Specification block | Fields to define | Why it prevents disputes |
|---|---|---|
| Product identity | SKU, material, attachment type, clip profile or strip format, finish, unit system, pack size, and revision | Prevents a generic report from being applied to a different configuration |
| Functional requirement | Nominal mass or increment, rim or surface context, retention method, application steps, and permitted variation | Connects the check to the way the product will actually be used |
| Appearance and pack | Coating coverage, burr and deformation limits, label fields, quantity, inner pack, carton, and storage requirement | Makes cosmetic and packing decisions observable rather than subjective |
| Evidence and release | Sample plan, instrument or fixture, photos, raw readings, lot code, deviation route, and approval owner | Shows who made the decision and what happens when a result is unclear |
For dimensions and unit increments, carry the exact values from the wheel weight size chart or the approved drawing into the purchase specification. Do not let the inspector choose a convenient unit after the goods arrive. An assortment can contain the correct total mass while still having the wrong segment mix, and a strip can have the correct length while using the wrong increments.
Resolve missing limits before production approval. Assign each open requirement to an owner; do not copy a number from another material, profile, or market.
What does a practical wheel weight QC matrix look like?
A practical matrix follows the physical and commercial path of the product: identify it, measure it, check attachment, inspect condition, verify the pack, and close the record. Every row should state the sample or scope, method, acceptance rule, evidence, and disposition.
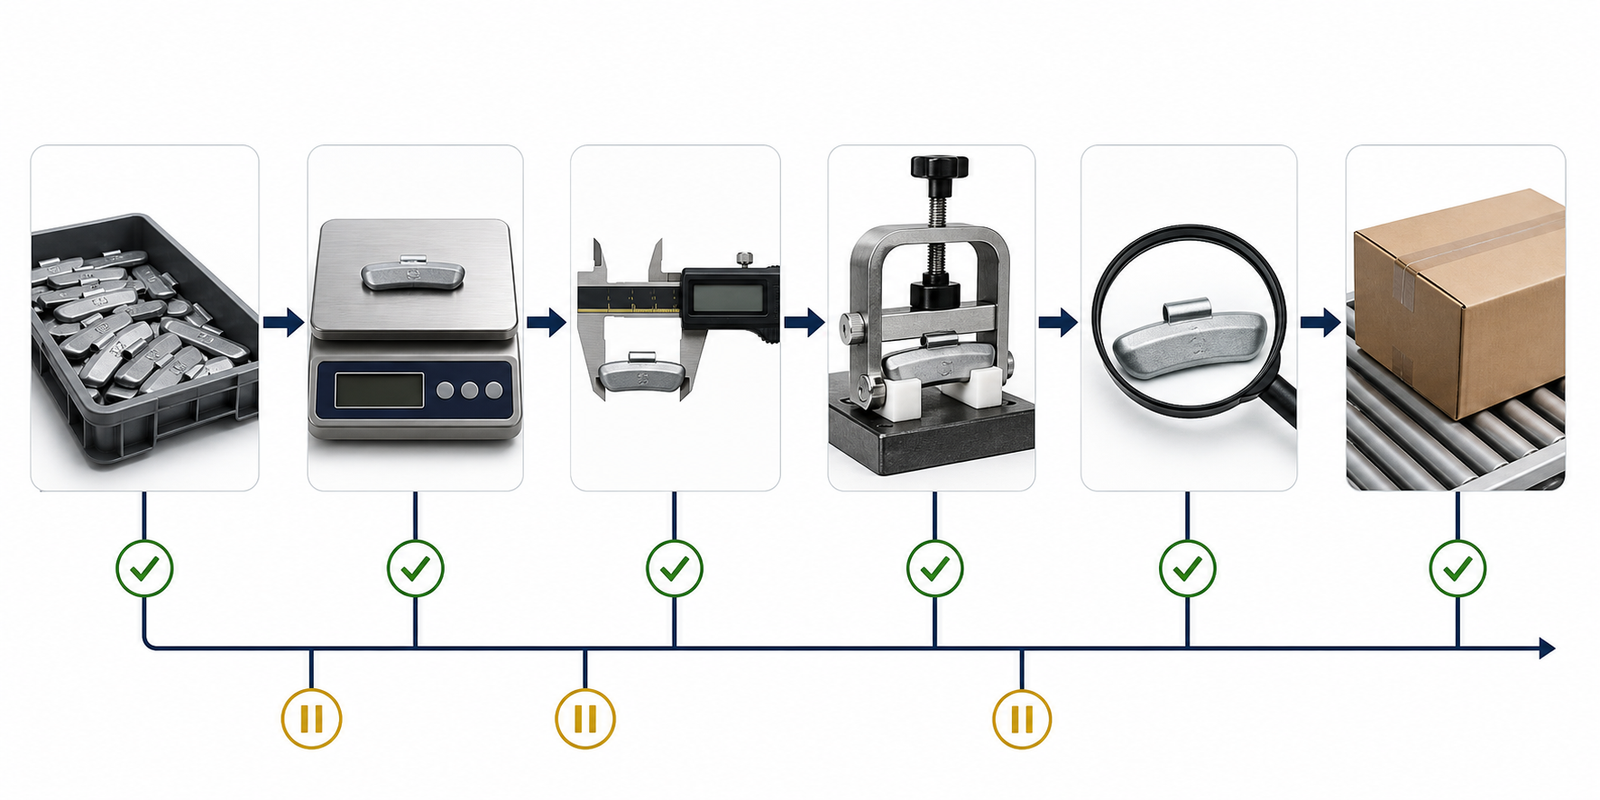
| Checkpoint | What to inspect | Evidence and release action |
|---|---|---|
| SKU identity | Match the part, label, carton, purchase order, approved sample, material, profile, and revision | Photos and identifiers; hold the lot when identity cannot be reconciled |
| Mass and increment | Measure the defined unit: individual piece, segment, strip, roll, or assortment | Raw readings, scale reference, sample selection; recheck or segregate under the agreed rule |
| Attachment | Check clip seating and retention, or tape identity, liner, preparation, pressure, and evaluation | Fixture or surface photos, sample IDs, method record; hold when the test context is missing |
| Finish and condition | Check coating coverage, burrs, deformation, corrosion signs, contamination, and functional interfaces | Comparison photos and defect log; accept, rework, or isolate against the approved limit |
| Packaging and labels | Check unit count, inner pack, carton, label, batch field, protection, and packing list | Carton and pack photos; release, relabel, re-pack, or quarantine |
| Record closure | Reconcile the report, revision, attachments, open findings, and final decision | Signed report and disposition owner; close findings through verified correction or an authorized, documented disposition before release |
Add product-specific limits and a sampling plan to this matrix. ISO 28590 introduces attribute-sampling systems; it does not supply a single sample count for every wheel-weight order.2
What should you enter on the QC record?
Use one header per lot and one result row per inspected unit or defined test group. Keep the observed value separate from the acceptance limit; a blank reading cannot count as a pass.
| Record field | Entry to make |
|---|---|
| Lot header | PO; SKU and revision; material; clip profile or tape identity; nominal increment and unit; lot size; carton range; inspection date |
| Sample selection | Sampling plan and revision; cartons or production positions selected; sample IDs; quantity checked per characteristic |
| Mass result | Unit inspected; nominal mass; agreed lower and upper limits; scale ID and resolution; individual readings; result |
| Dimension result | Drawing revision; feature measured; permitted range; gauge ID; individual readings; result |
| Attachment result | Rim or panel identity; clip/tape lot; preparation; application conditions; fixture and loading direction; evaluation time; observation or force reading |
| Defect and closure | Sample/carton ID; requirement not met; photograph or raw-data file; affected scope; hold/rework/reject/deviation decision; recheck result; approver and date |
For an attribute-sampling plan, record the inspection level, AQL where applicable, sample size, and acceptance/rejection numbers from the selected plan. Define which observations count as defects before counting them. Use the specified measurement rule for mass and dimensions; do not assume an AQL label itself supplies a numerical tolerance.2 Select samples across the defined lot rather than letting the supplier present only its best pieces.
How should weight, markings, and dimensions be checked?
Compare individual measurements with the approved limits. Check markings against the SKU, unit system, and pack specification separately from the scale reading.
Record the tolerance for the exact inspection unit and nominal increment in the approved specification, together with any applicable standard or customer requirement. A strip total cannot establish that every segment has the correct mass. Confirm the balance resolution and measurement method before judging readings near a limit.
Use this sequence for the weight and identity check:
- Define the inspection unit. State whether one piece, one segment, one strip, one roll, or one complete assortment is being measured.
- Confirm the reference. Record nominal mass, increment, unit system, SKU, revision, and any permitted variation from the approved specification.
- Control the measurement. Record the scale or gauge reference, suitable resolution, condition, sample selection, and responsible inspector.
- Compare the result. Record raw readings rather than only “pass,” especially when an assortment or strip can hide an incorrect internal mix.
- Reconcile the marking. Compare product markings, inner-pack labels, carton labels, and packing-list fields with the same approved identity.
For clip-on weights, measure the clip and rim-interface features called out on the approved drawing, using the specified reference rim or fixture for fit checks. For adhesive weights, check segment length, width, body thickness, total thickness including tape, and spacing where specified. Measure each feature against its own limit; a correct mass does not establish caliper clearance or clip fit. Keep the drawing revision and gauge reference beside the readings.
Markings should be legible for the intended service workflow. A grams-based pack must not be presented in a way that a technician can mistake for ounces. Where small items do not carry individual markings, the inner pack and carton must identify the product clearly enough for receiving, storage, and installation.
How should clip retention and adhesive tape be checked?
Use the specified rim or representative surface, preparation, loading method, evaluation time, and failure definition. An informal hand pull or stick test cannot substitute for that record.
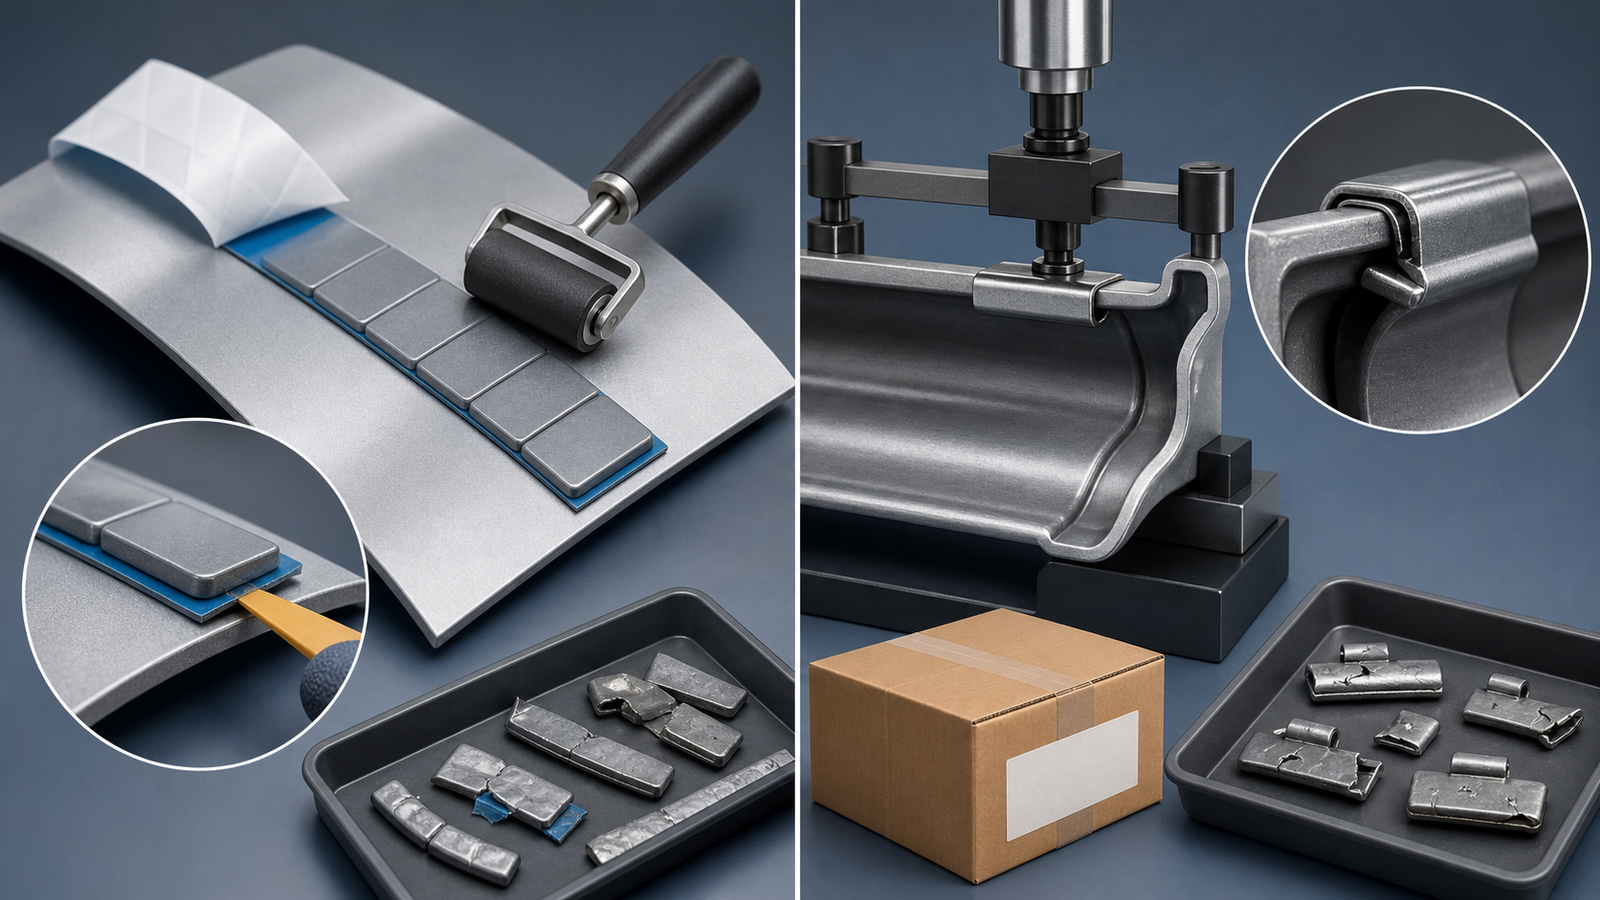
How should clip-on wheel weight retention be checked?
Match the exact clip profile to the intended rim or flange geometry, then record the fixture or reference wheel, loading direction, force or test method, sample count, and failure definition. Note whether the clip remains seated, whether the coating or clip deforms, and whether the result applies only to that profile or to an approved family.
SAE J1986 provides a reference for balance-weight and rim-flange features, configurations, retention testing, and minimum performance requirements for relevant vehicle applications 1. Use the current applicable revision and the actual target wheel context. A result on one clip profile does not prove fit on every wheel.
Confirm the clip-on profile and rim application before testing. Record the sample IDs, fixture, clip and coating condition, method, and result.
How should adhesive wheel weight tape be checked?
For adhesive products, verify the tape identity, liner release, strip condition, segment separation, intended wheel surface, cleaning method, application temperature, pressure, dwell, evaluation time, and detachment or edge-lift rule. The adhesive wheel weight formats should not be approved from a tape sample that is different from the production configuration.
3M application guidance treats substrate preparation, contact pressure, and dwell as important parts of pressure-sensitive adhesive application.3 Its wheel-weight application document also calls for checking contact area, contamination, coating compatibility, application temperature, and placement across wheel features.6 Those instructions apply to the specified 3M system; use the actual tape supplier’s instructions for another construction.
For a formal retention requirement within its scope, ISO 13988:2021 covers clip and adhesive balance-weight configurations, test procedures, and minimum retention performance.5 Name the applicable standard, revision, test, and product configuration in the order. Do not replace that requirement with an improvised hand pull or transfer a pressure, temperature, or force limit from an unrelated tape.
What should you check when adhesive weights fall off?
Keep the detached weight and photographs of the wheel, tape, and liner where available. Record where separation occurred before cleaning away the evidence. Check the installation conditions against the tape instructions before deciding whether the complaint concerns the supplied product or the fitting process.6
| Complaint observation | QC comparison to make |
|---|---|
| Poor contact or edge lift | Compare wheel curvature and coating, placement, application pressure, and the agreed contact-area check. |
| Failure after a cold installation | Record wheel and weight temperatures, dryness, and time before evaluation; compare with the product’s application conditions. |
| Tape or residue remains on one surface | Photograph both mating surfaces and identify the separation interface; compare retained units from the same tape and weight lot under a controlled method. |
| Several complaints from one box or lot | Trace the affected units, tape identity, storage, coating, and fitting records. Hold the suspect scope while the cause and disposition are reviewed. |
These observations direct the investigation; none identifies the cause by itself. Retest retained units and a comparison sample under the same documented conditions. Avoid treating a clean-panel result as approval for a different wheel coating or using extra tape to hide a failed acceptance check.
What should finish, packaging, and traceability inspection cover?
Finish inspection should compare the defined visible and functional surfaces with an approved sample, photo set, or written defect limit. Packaging and traceability inspection should then prove that the accepted product remains identifiable and usable when it enters inventory or leaves the factory.
For finish and physical condition, check coating coverage, edges, clips, burrs, deformation, corrosion signs, contamination, sharp projections, liner damage, and coating damage at functional interfaces. Separate normal manufacturing texture from defects that the specification actually defines as unacceptable. A vague demand for “perfect appearance” creates arguments; a reference photo and defect limit create a decision.
For coated steel, the coated steel corrosion-test evidence should be kept separate from a routine visual check. ASTM B117-26 describes a controlled salt-spray environment, but it does not prescribe the specimen, exposure period, or interpretation for a particular product, and salt-spray results do not automatically predict natural service life 4. Define the samples, method, duration, and acceptance criteria before requesting a corrosion report.
Packaging and label checks should cover:
- SKU, revision, material, profile or strip format, and unit system.
- Quantity per inner pack and carton, including mixed-SKU separation.
- Liner and strip protection, clip protection, carton condition, and moisture handling.
- Batch, carton, date, or packing references used by the quality and logistics records.
- Packing-list agreement and photographs of any damaged, relabeled, or opened carton.
The wheel weight packaging and label checks are especially useful when close-looking SKUs share one shipment. The wheel weight traceability records should connect the carton or batch to the approved configuration, inspection result, and supporting document. If a label is missing or inconsistent, isolate the carton instead of assigning an identity from appearance alone.
What happens when an inspection result fails?
When a result fails or cannot be interpreted, contain the affected stock first and clarify the evidence second. Identify the SKU, lot, carton, or packing group; separate it from approved stock; preserve the sample and photographs; and state the observation against the agreed rule.
| Finding | Immediate action | Release evidence |
|---|---|---|
| Wrong SKU, label, or revision | Hold affected cartons and reconcile the product, label, and order records | Corrected identity with responsible approval |
| Weight or increment concern | Quarantine the affected unit or lot and review measurement method and sample selection | Raw recheck results against the same specification |
| Clip or tape concern | Stop normal release and repeat under the defined profile, surface, and preparation | Controlled test record and disposition |
| Finish or corrosion concern | Retain comparison samples and separate routine appearance from special testing | Approved visual or test criterion with result |
| Quantity or pack mismatch | Hold cartons, count the defined scope, and protect SKU separation | Corrected count, label, or packing record |
Do not quietly blend suspect stock with accepted stock. The buyer and supplier should agree who can authorize release, rework, replacement, or deviation, then record that decision against the same lot identifier used on the inspection report. A general promise to “improve quality” is not a disposition.
Do not resample repeatedly until a failed lot passes. Follow the rejection, containment, correction, and reinspection rules of the selected plan. Keep the first result in the record and identify any reworked units separately.
If the issue is recurring, compare the evidence across sample approval, production QC, and shipment release. The pattern may point to a changed clip profile, uncontrolled tape storage, mixed packaging, an instrument problem, or an unclear acceptance rule. Fix the control point that produced the uncertainty instead of adding another unverified inspection line.
What evidence should the buyer request before release?
Request the specification, inspection results, supporting files, and signed disposition for the identified lot. Another reviewer should be able to follow the release decision from those records.
The package should normally contain:
- The purchase order, product specification, approved sample reference, and revision.
- SKU, material, attachment format, profile, unit system, pack, lot, and carton identifiers.
- The sampling plan, sample selection method, inspection stage, and acceptance rule.
- Raw mass readings, dimensional observations, clip or tape test details, and instrument or fixture references.
- Comparison photos for product condition, labels, packaging, and any nonconforming finding.
- Batch, carton, packing-list, and certificate records where the order requires them.
- The final release, recheck, rework, replacement, or deviation decision with owner and date.
When evaluating a new source, the wheel weight manufacturer controls matter because a strong sample cannot compensate for weak change control or missing lot records. Ask what happens when a material, coating, tape, clip, tool, label, or packing method changes. The answer should lead to a new sample, review, or retest when the agreed risk requires it.
If you need a product-specific matrix, send the target SKU, attachment format, profile or wheel context, nominal increments, packaging plan, destination market, expected volume, and current supplier evidence with your wheel weight QC review request.
Conclusion: Make every release decision traceable
Wheel weight QC works when every important check is tied to the supplied product: the correct SKU, agreed mass or increment, suitable clip or tape evaluation, defined finish criteria, accurate labels and packs, and retrievable lot evidence. The value is not the number of boxes marked “pass”; it is the ability to explain why the goods were released.
Before production, agree the product identity, sample plan, method, acceptance rule, evidence, and disposition route. Keep the approved sample and packaging reference with the inspection record, then connect that record to the shipment. That sequence gives buyers a repeatable way to control fitment, balance correction, packaging, and repeat-order consistency.
Frequently Asked Questions
What is the most important wheel weight QC check?
Product identity comes first. Once the SKU, revision, attachment format, and unit system are confirmed, check the characteristics that affect use: mass or increment, clip fit or tape condition, finish, labeling, packaging, and traceability.
Is there one universal wheel weight tolerance?
No. The tolerance depends on the product format, nominal increment, measuring method, customer requirement, and intended market. Put the limit in the approved product specification and record the method used to verify it.
Can a supplier inspection sheet replace sample approval?
No. A supplier sheet can support the file, but the buyer still needs an approved sample or specification that defines the product, method, and acceptance criteria. Without that reference, a “pass” result is difficult to interpret.
How should adhesive wheel weight tape be tested?
Use the actual tape and liner on the intended or defined representative wheel surface. Record cleaning, surface condition, temperature, pressure, dwell, evaluation time, edge lift, contamination, liner release, and the agreed pass condition.
What should happen to a mislabeled wheel weight carton?
Hold it outside normal inventory, retain the label and shipment evidence, and verify the identity through controlled records. Do not merge it with similar-looking stock until the SKU, quantity, and batch or carton reference are reconciled.
Why do adhesive wheel weights fall off soon after fitting?
Check contamination, incomplete contact, coating compatibility, placement, and wheel and weight temperatures against the actual product’s instructions. The 3M wheel-weight troubleshooting procedure includes these checks, but its application limits belong to that system.6 A fresh installation failure alone does not prove defective tape.
For a supplier-quality complaint, retain the detached parts, photograph both surfaces, identify the tape and weight lot, and record preparation, pressure, temperature, and evaluation time. Compare retained samples under the same conditions before attributing the failure to installation or the supplied lot. Do not approve a suspect lot from a successful stick test on an unrelated panel.
References
[1] SAE International. “J1986: Balance Weight and Rim Flange Design Specifications, Test Procedures, and Performance Recommendations.” 2016; check current revision.
[2] ISO. “ISO 28590:2017 — Sampling procedures for inspection by attributes.” 2017.
[3] 3M. “General Installation Techniques for Pressure-Sensitive Adhesives.” 2024.
[4] ASTM International. “B117: Standard Practice for Operating Salt Spray (Fog) Apparatus.” 2026.
[6] 3M. “3M Wheel Weight System: Application Guidelines for Wheel Balancing and Equipment.” January 2026.