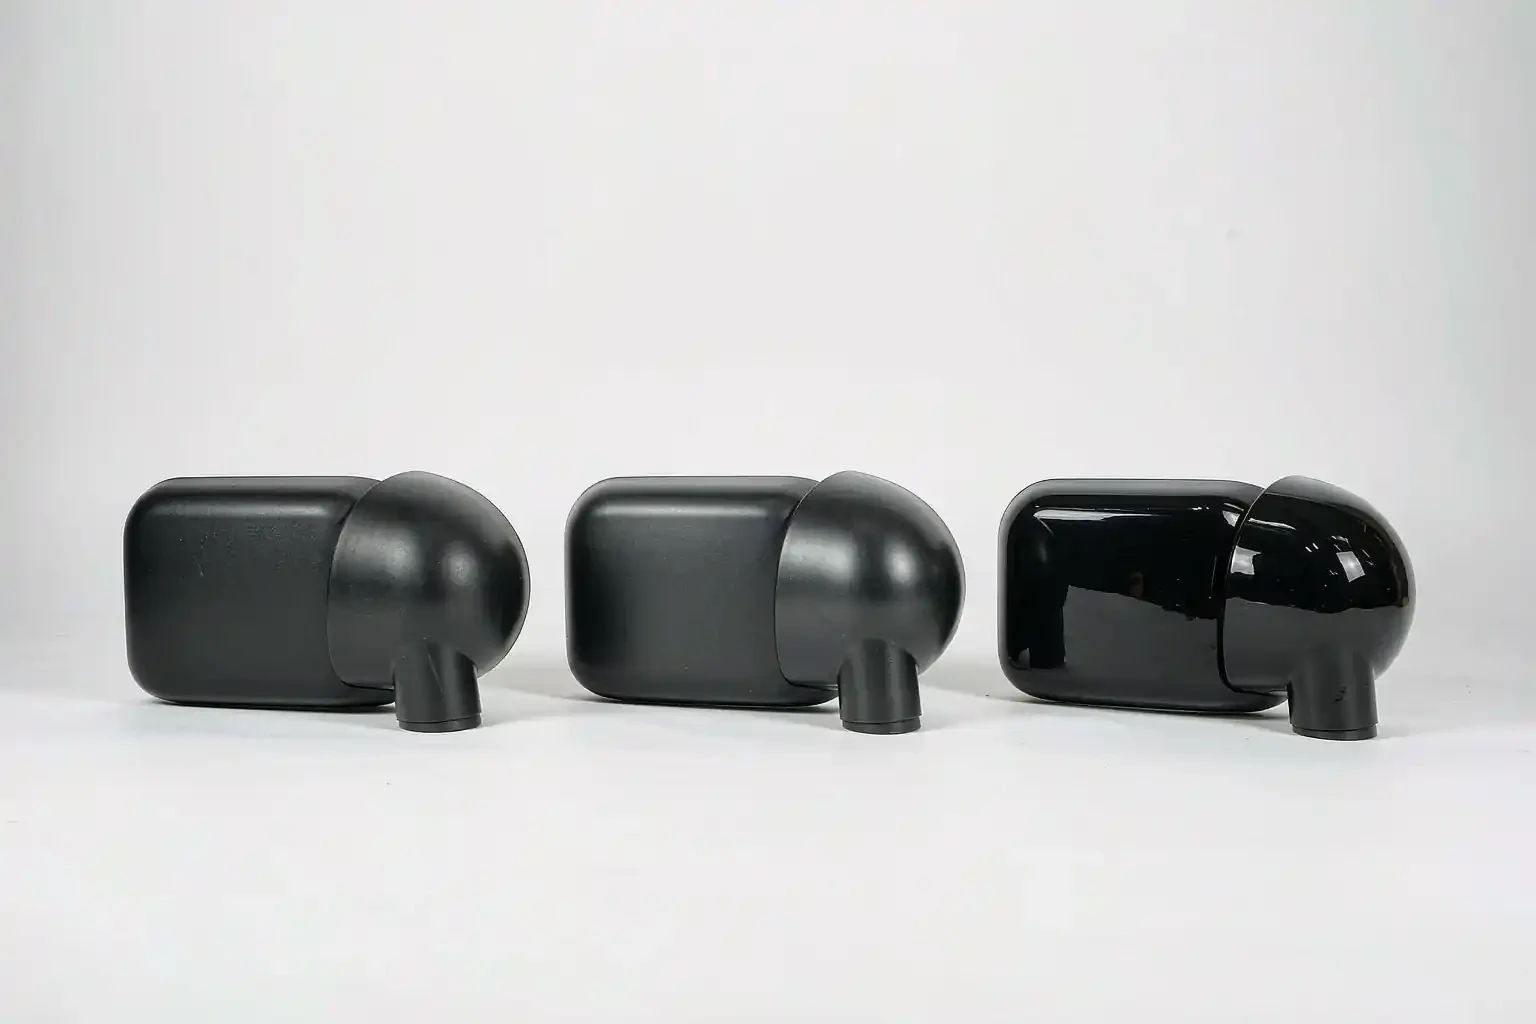
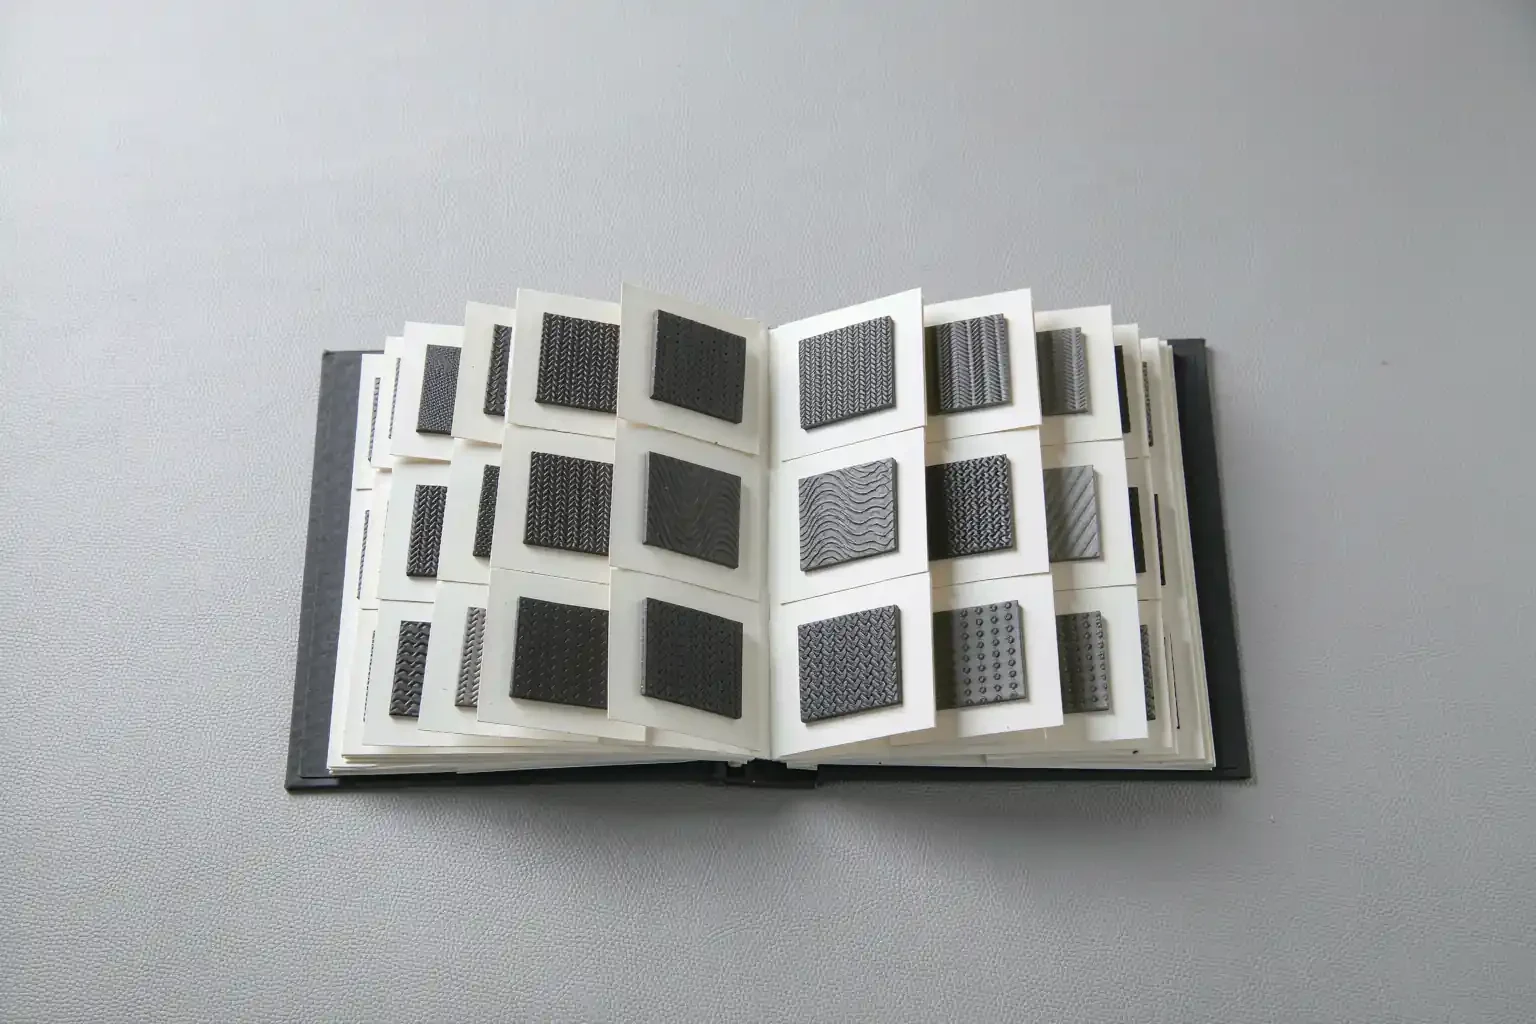
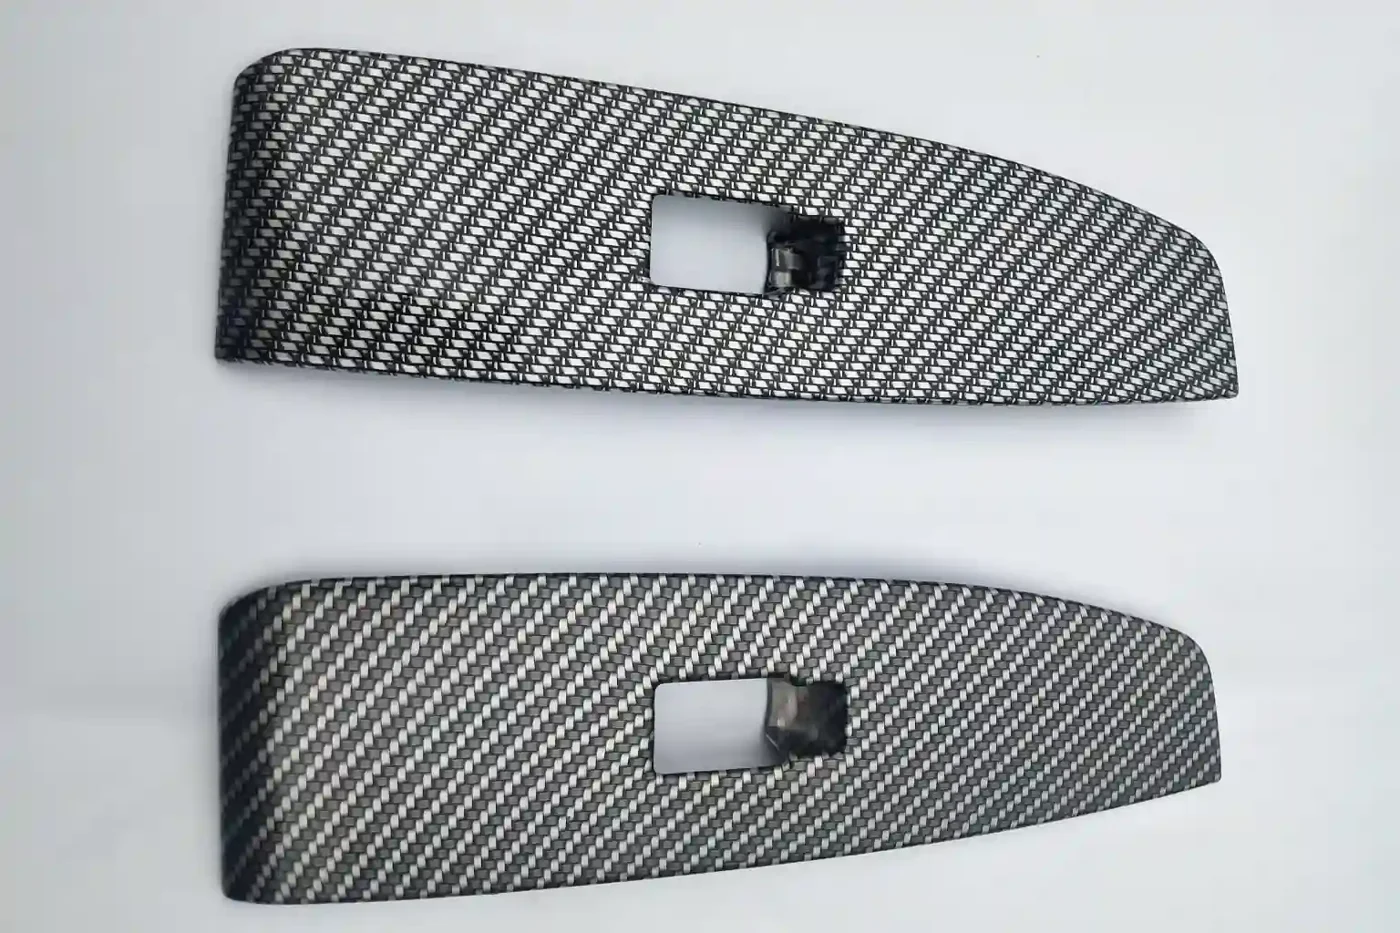
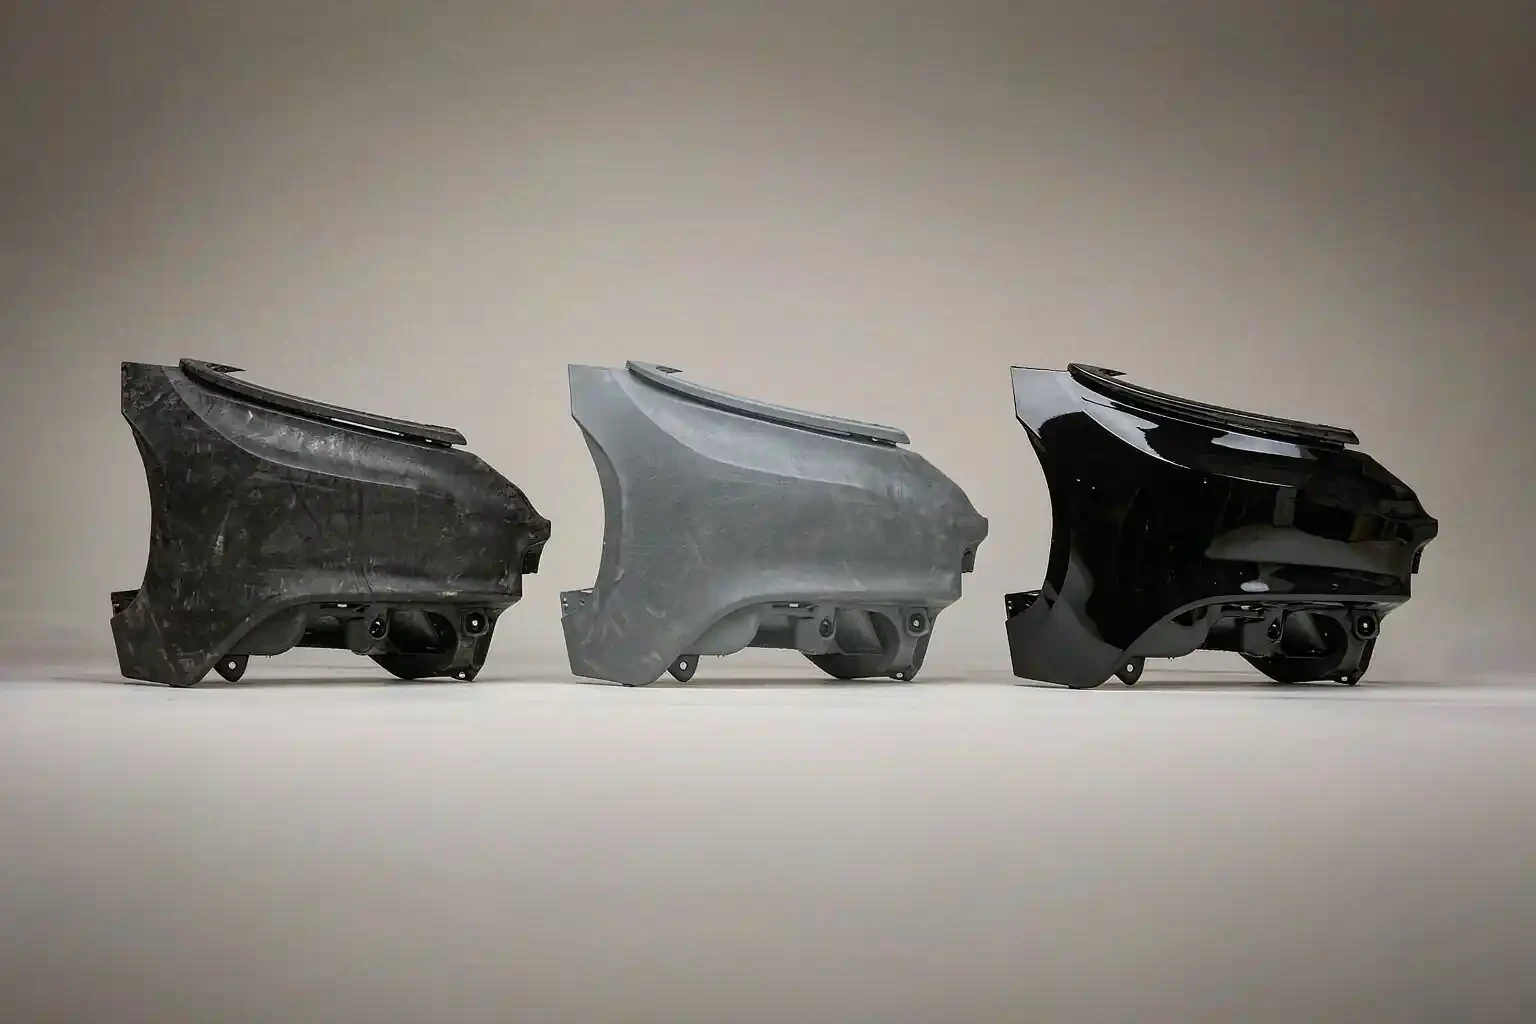
A practical guide to the plastics and finishes used on automotive exterior parts: ABS, PC/ABS, ASA, PP and TPO, two-shot materials, piano black, matte, texture, carbon look, primer and chrome. Each page explains the material or finish, how Yirox uses it, and what we can make in our IATF 16949 factory in Wuxi.

| Group | Pages | Typical exterior parts |
|---|---|---|
| Rigid styling plastics | ABS, PC and PC/ABS, ASA | Grilles, mirror caps, spoilers, front lips, trim |
| Impact and bumper plastics | PP and TPO | Bumpers, fender flares, side skirts, mud flaps |
| Two-shot materials | PC+PMMA, ABS+TPE, PC/ABS+TPU | Clear-over-black trim, soft-edge covers and seals |
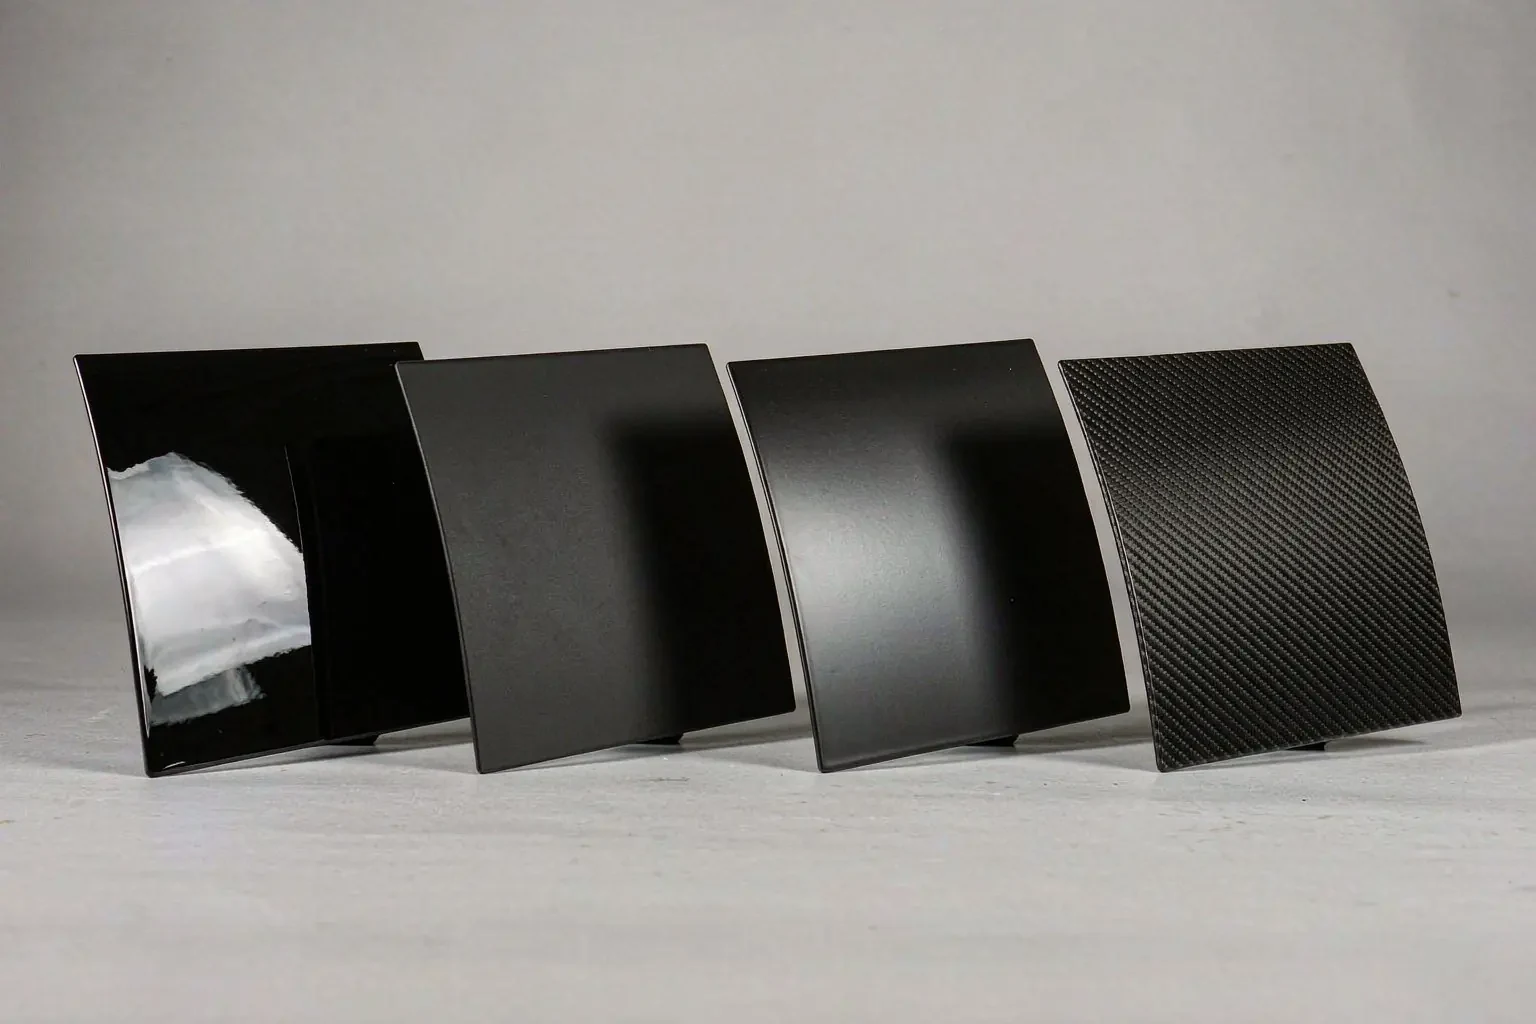
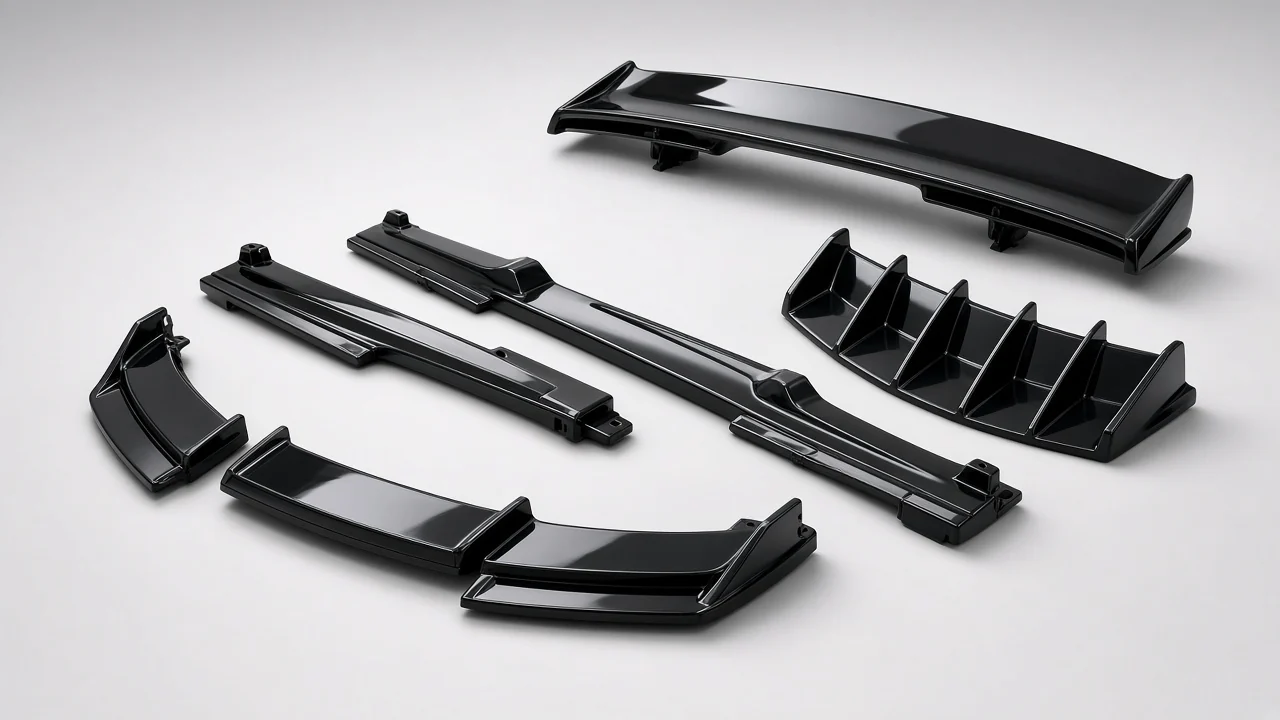
| Paint finishes | Piano black and gloss black, matte and satin black | Spoilers, mirror caps, diffusers, trim |
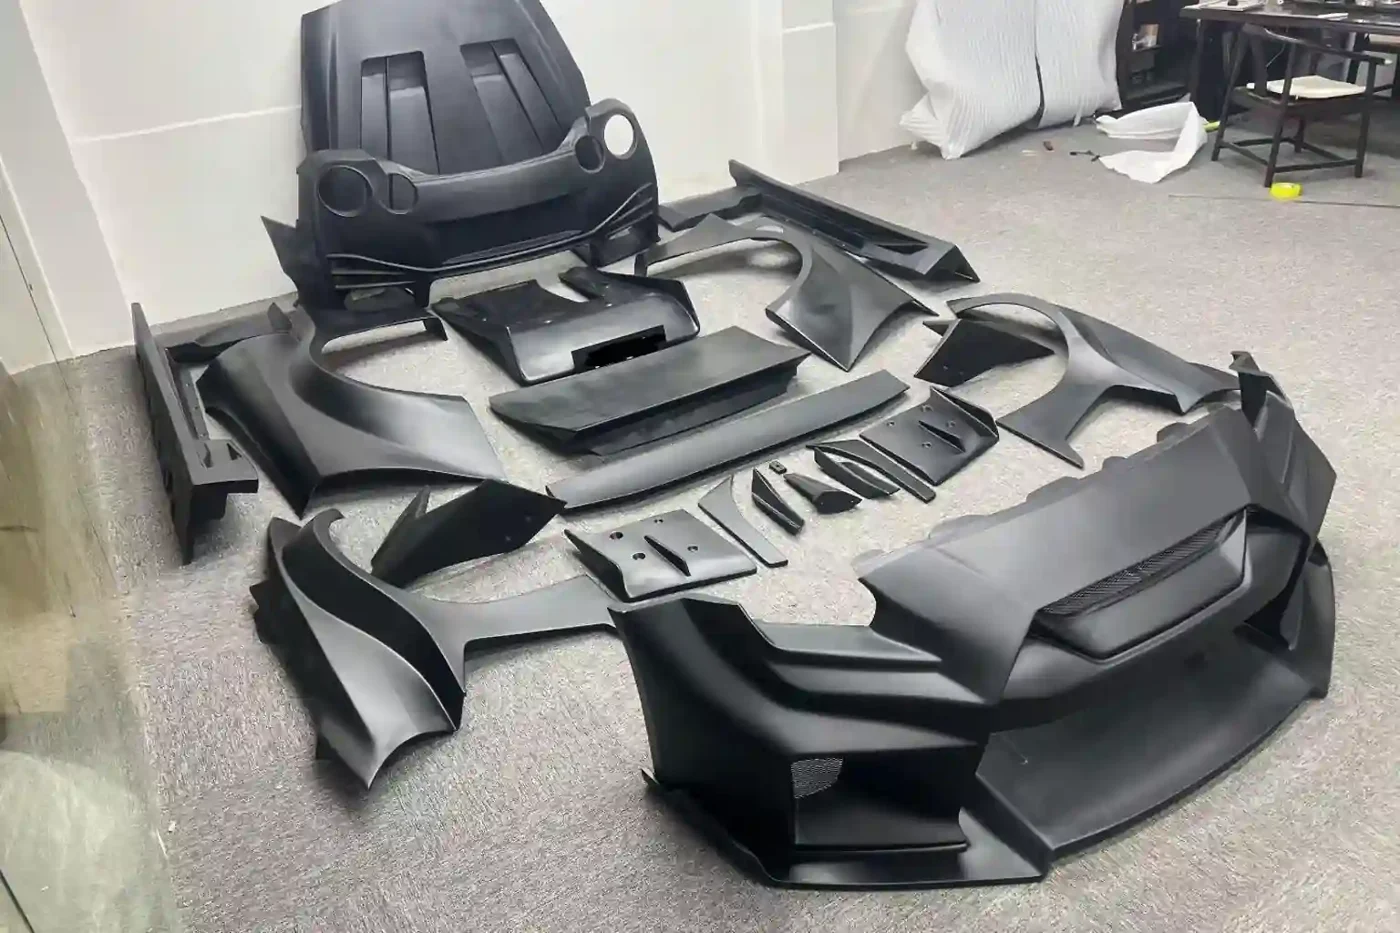
| Molded and decorative finishes | Mold texture, carbon fiber look, primed, painted and molded-in color | Fender flares, louvers, covers, body kits |
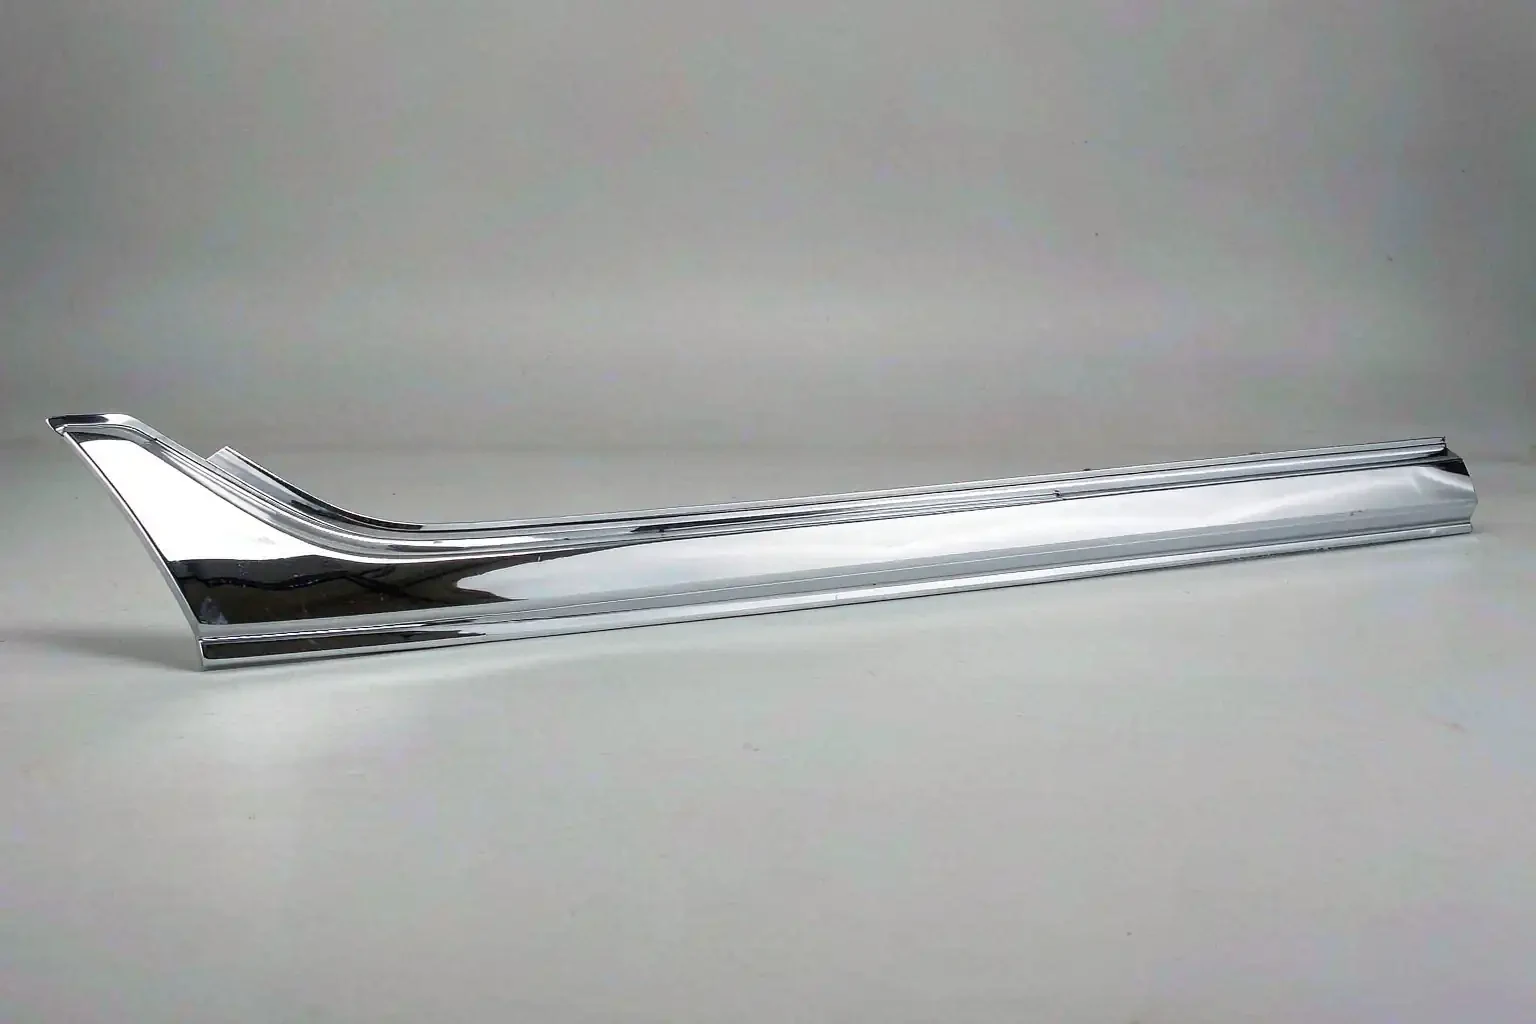
| Metal finish | Chrome plating on plastic | Grille bars, trim strips, handle covers |
Five material groups, plus partner composites, cover almost every exterior plastic part we make. Each page explains the material, its typical properties and the parts we mold from it.

Rigid, easy to paint and the standard plating-grade plastic. Used for grilles, mirror caps, spoilers and body kits.
Learn more →
Higher heat and impact than ABS. Used for mirror housings, larger rigid trim and two-shot parts.
Learn more →
UV-stable, holds color outdoors without paint. Used for textured louvers, pillar trim and grille surrounds.
Learn more →
Tough and flexible in the cold, the main bumper material. Used for bumpers, flares, side skirts and mud flaps.
Learn more →
PC+PMMA, ABS+TPE and PC/ABS+TPU joined in one cycle on 3 two-shot machines. Clear-over-black trim and soft edges.
Learn more →
Real carbon fiber and fiberglass parts made by partner composites factories. Compare them with ABS for spoilers.
Learn more →Five finish families, plus chrome plating on ABS. Each page gives the gloss targets, how the finish is made and where it is used.

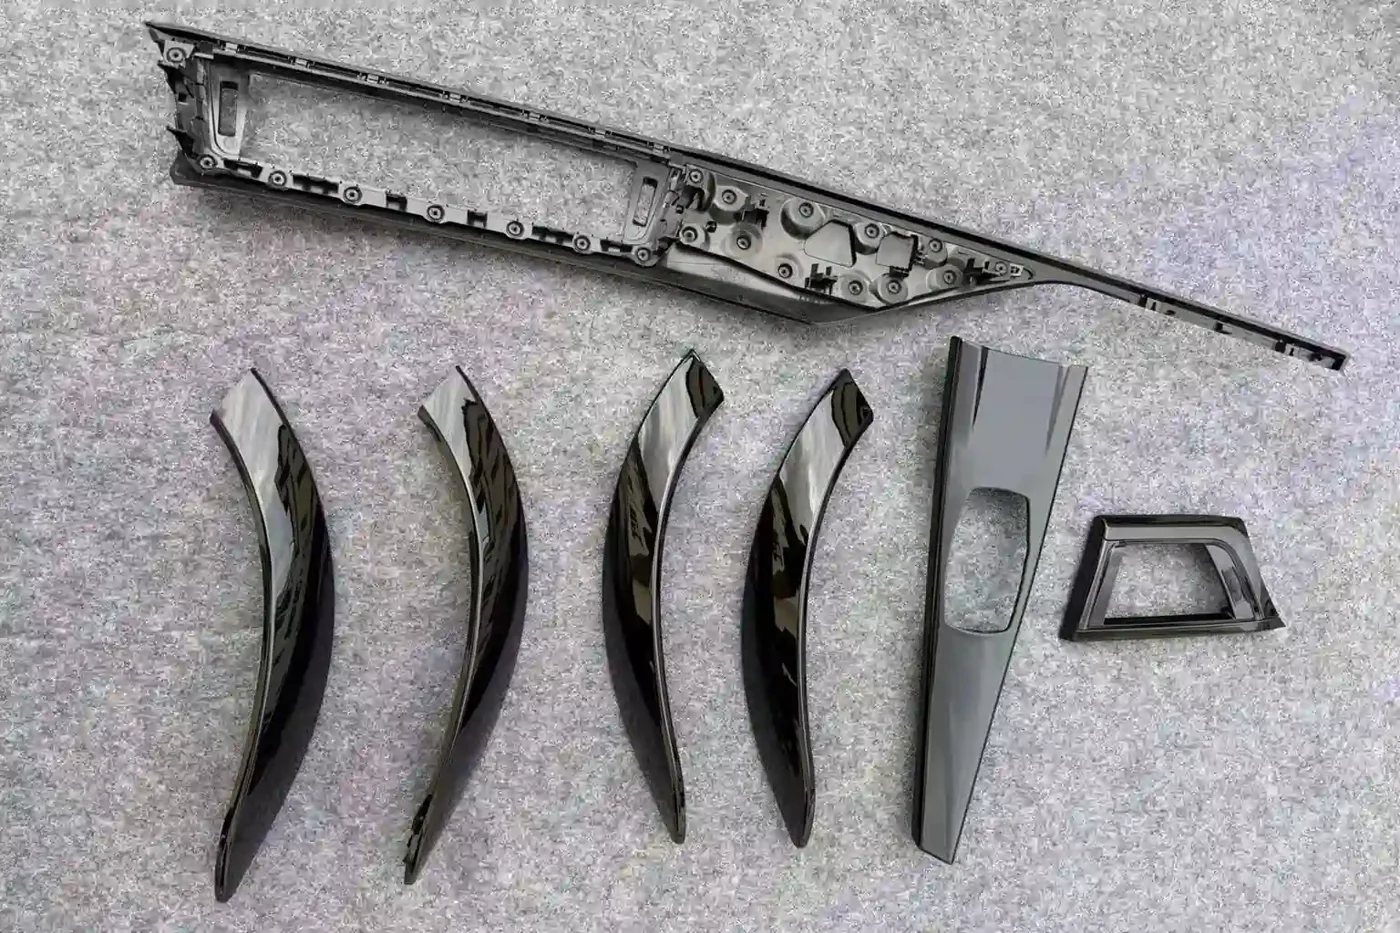
Piano black ≥95 GU and gloss black ≥90 GU at 60°, painted 3C2B in ISO 7/8 clean rooms. Spoilers, mirror caps, trim.
Learn more →
Matte 5–15 GU and satin 20–40 GU at 60°, painted or molded paint-free. Checked at 60° and 85°.
Learn more →
VDI 3400, SPI A1–D3, leather grain, fine sand and bead-blast. Grain gloss 2–6 GU; texture plaques for approval.
Learn more →
Water transfer printing with UV-cured clear, IMD or film, and real carbon fiber through partner factories.
Learn more →
Molded-in color (3–8 GU), primed with PP/TPO adhesion primer, or fully painted 3C2B color plus clear.
Learn more →
Cu/Ni/Cr ≥32 μm on plating-grade ABS, trivalent chrome, CASS 48 h. Grilles, trim strips and emblems.
Learn more →Automotive plastics are the engineering polymers used to make vehicle parts that once were made of steel, glass or rubber. On the exterior of a modern car, plastic is used for bumpers, grilles, mirror housings, spoilers, wheel arch trim, side skirts, cladding and dozens of clips and brackets.
Plastic parts weigh less than metal, do not rust, can be molded into complex shapes in one step, and can be painted, textured or plated to match any styling.
Most exterior parts are made from a small group of thermoplastics. ABS and PC/ABS are used for rigid styling parts that will be painted or plated. ASA is used where the part stays unpainted in the sun. PP and TPO are used for bumpers and other large parts that must survive impacts and cold weather. Two-shot combinations add a clear layer or a soft edge in one molding cycle.

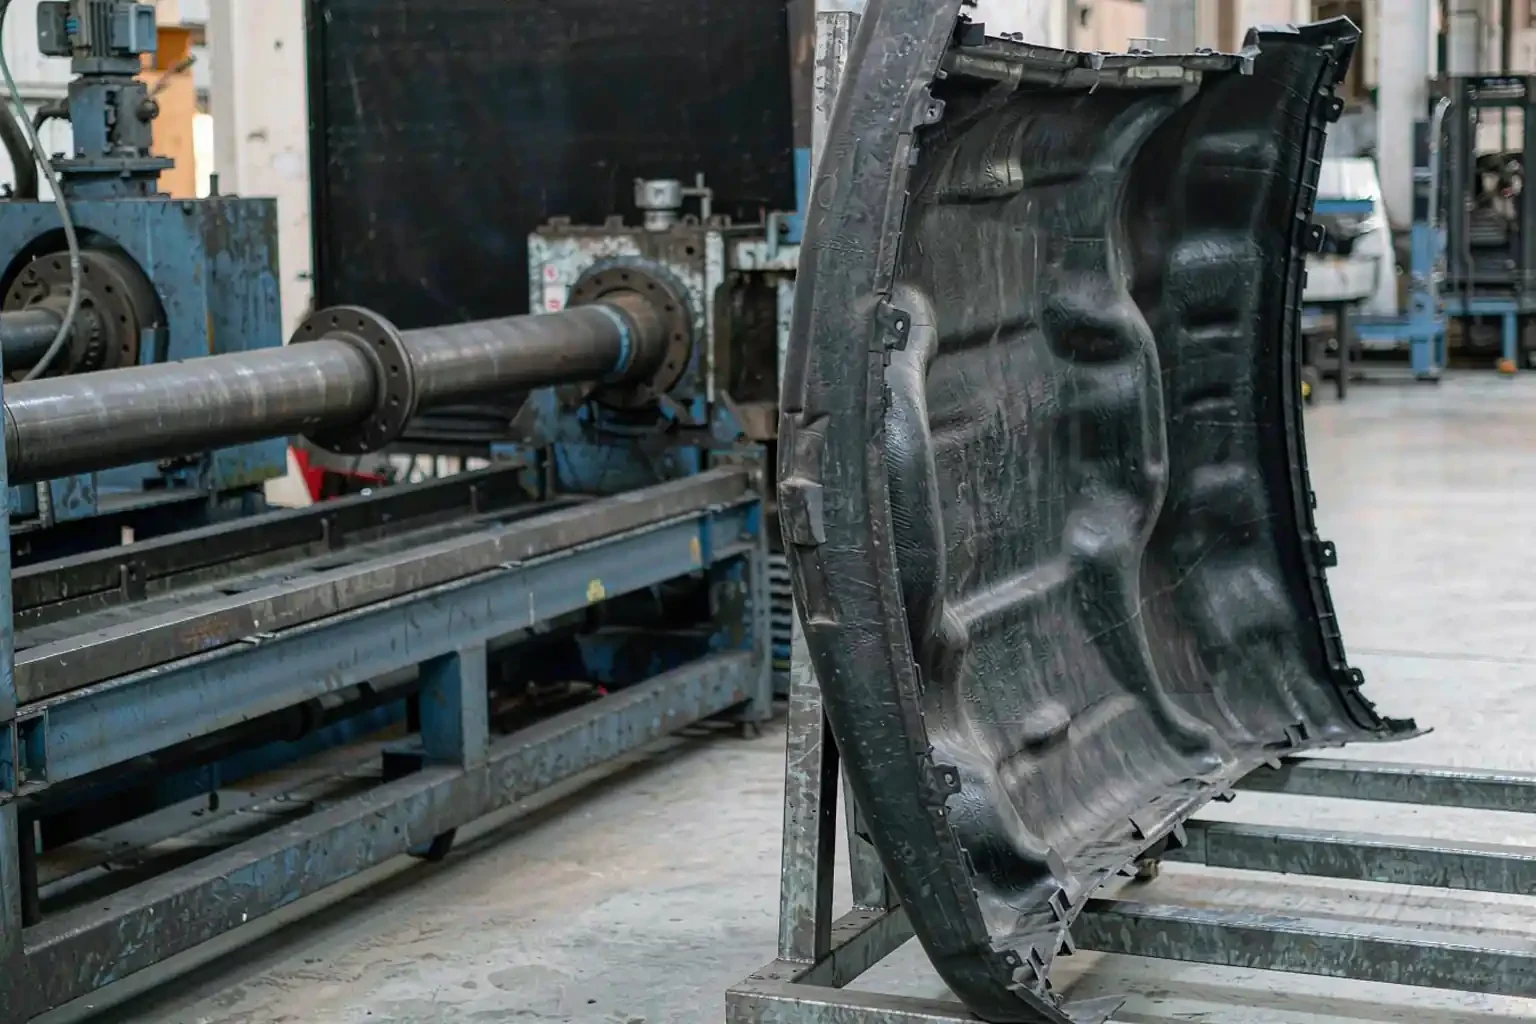
Most modern car bumper covers are made of polypropylene compounds, usually talc-filled PP or TPO. These materials are tough at low temperature, flex on impact and return to shape, and cost less than engineering plastics. The bumper cover is painted to body color after an adhesion primer is applied. Behind the cover, an energy absorber of foam or plastic and a metal reinforcement beam take the crash load.

Aftermarket bumper parts such as front lips, diffusers and bumper trim are often made from ABS or PC/ABS instead, because these parts are smaller, stiffer and are usually finished in piano black, matte black or a carbon look.

| Part | Common material | Why | Typical finish |
|---|---|---|---|
| Front and rear bumper covers | PP / TPO (talc-filled) | Impact at low temperature, flexibility | Primer + body color paint |
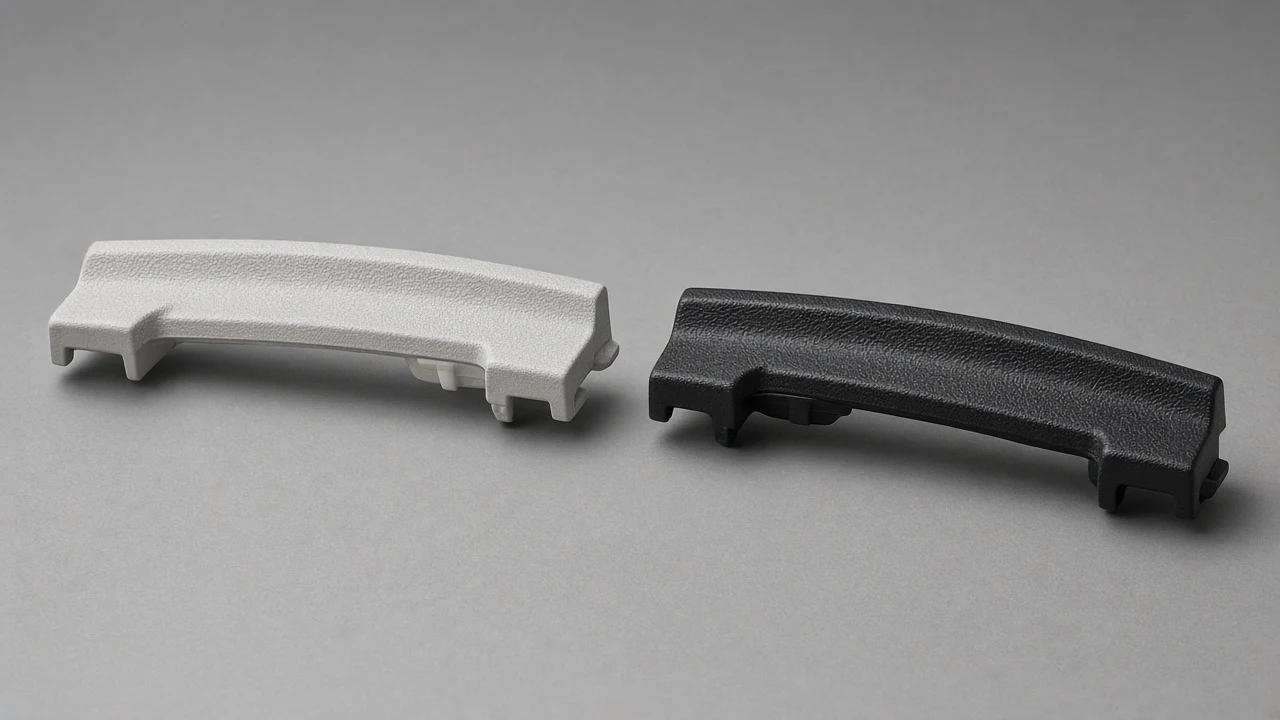
| Fender flares and wheel arch trim | PP / TPO or ASA | Impact, unpainted weathering | Molded-in color with texture |
| Grilles and grille surrounds | ABS, PC/ABS, plating-grade ABS | Stiffness, detail, paint or chrome | Piano black or chrome |
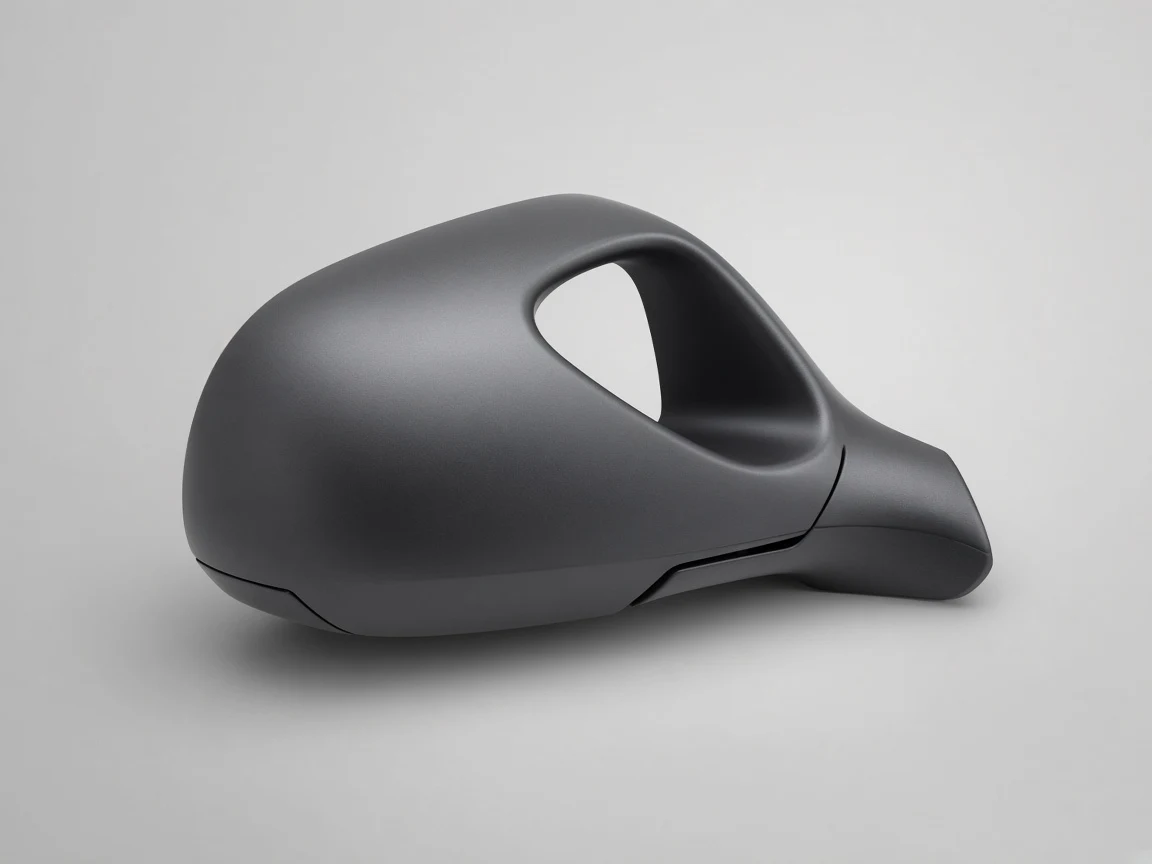
| Mirror caps and housings | ABS, PC/ABS | Surface quality, heat resistance | Gloss black, carbon look, body color |
| Spoilers and wings | ABS, PC/ABS | Stiffness and surface for paint | Gloss black, matte black |
| Front lips, side skirts, diffusers | ABS, PP | Impact and flex near the road | Gloss or matte black, MIC |
| Window louvers and pillar trim | ASA, ABS | UV stability, flatness | Textured MIC, piano black |
| Mud flaps and splash guards | PP, TPO, TPE | Flexibility | Molded-in color |
| Wheel covers and center caps | ABS, PC/ABS | Detail and finish | Paint, chrome or MIC |
This table shows which finishes we usually combine with each material. “On request” means it is possible in principle and is confirmed by sample for your part.
| Material | 3C2B paint (gloss) | Matte / satin paint | Molded-in color + texture | Chrome plating | Water transfer carbon | Primed only |
|---|---|---|---|---|---|---|
| ABS | Yes | Yes | Yes, mainly hidden or interior-side parts | Plating-grade ABS only | Yes | Yes |
| PC/ABS | Yes | Yes | Yes | No (ordinary PC/ABS not suitable) | Yes | Yes |
| ASA | Yes | Yes | Yes, best for unpainted exterior parts | No | On request | Yes |
| PP / TPO | Yes, with PP/TPO adhesion primer | Yes, with adhesion primer | Yes | No | Yes, after primer | Yes, PP/TPO adhesion primer |
| Two-shot PC+PMMA | Usually unpainted | No | Black base + clear top | No | No | No |
Gloss is measured in gloss units (GU) with a gloss meter. We check gloss with a BYK micro-TRI-gloss meter at 20°, 60° and 85°. The 60° values below are our standard targets. High-gloss parts are also checked at 20° for distinctness of image (DOI), and matte parts at 85°. Values measured at different angles cannot be compared with each other.

| Finish | Gloss at 60° | Extra check |
|---|---|---|
| Piano black | ≥95 GU | 20° / DOI |
| Gloss black | ≥90 GU | 20° / DOI |
| Satin black | 20–40 GU | — |
| Matte black | 5–15 GU | 85° |
| Grain texture | 2–6 GU | 85° |
| Molded-in color (MIC) | 3–8 GU | 85° |
Start with the environment of the part, then the finish, then cost. Ask these questions:

Painted parts can use ABS, PC/ABS or PP/TPO. Chrome needs plating-grade ABS.
Use UV-stabilized ASA, or a weather-stable PP/TPO compound.
Bumpers, flares and lips near the road suit PP, TPO or tough ABS grades.
PC/ABS has higher heat resistance than ABS for larger parts and dark colors.
Two-shot PC+PMMA, ABS+TPE or PC/ABS+TPU combine two materials in one part.
Molded-in color and texture remove the paint step. Piano black and chrome cost more but sell at a higher price.
These are typical published datasheet ranges for unfilled general-purpose grades, collected from resin manufacturers’ technical data sheets. They are for comparison only and are not Yirox test results. Exact values depend on the grade chosen for your part.
| Property | ABS | PC/ABS | ASA | PP copolymer | TPO |
|---|---|---|---|---|---|
| Density (g/cm³) | 1.03–1.07 | 1.10–1.17 | 1.06–1.08 | 0.90–0.91 | 0.95–1.05 |
| Tensile strength (MPa) | 38–50 | 45–60 | 40–50 | 20–30 | 15–25 |
| Notched Izod impact (J/m) | 200–400 | 400–700 | 100–300 | 80–500 | 400–no break |
| Heat deflection at 0.45 MPa (°C) | 90–100 | 110–130 | 90–100 | 85–100 | 80–100 |
| Mold shrinkage (%) | 0.4–0.7 | 0.5–0.7 | 0.4–0.7 | 1.2–2.0 | 0.8–1.2 |
| UV resistance unpainted | Poor | Fair | Excellent | Fair with stabilizer | Good with stabilizer |
We review the part, finish and use, and recommend a material family and grade type at the DFM stage.
Resin is dried in our 30 desiccant dryers and molded on 42 machines from 90 to 2,500 t.
Parts for paint are cleaned, pre-treated and primed; PP and TPO get an adhesion primer.
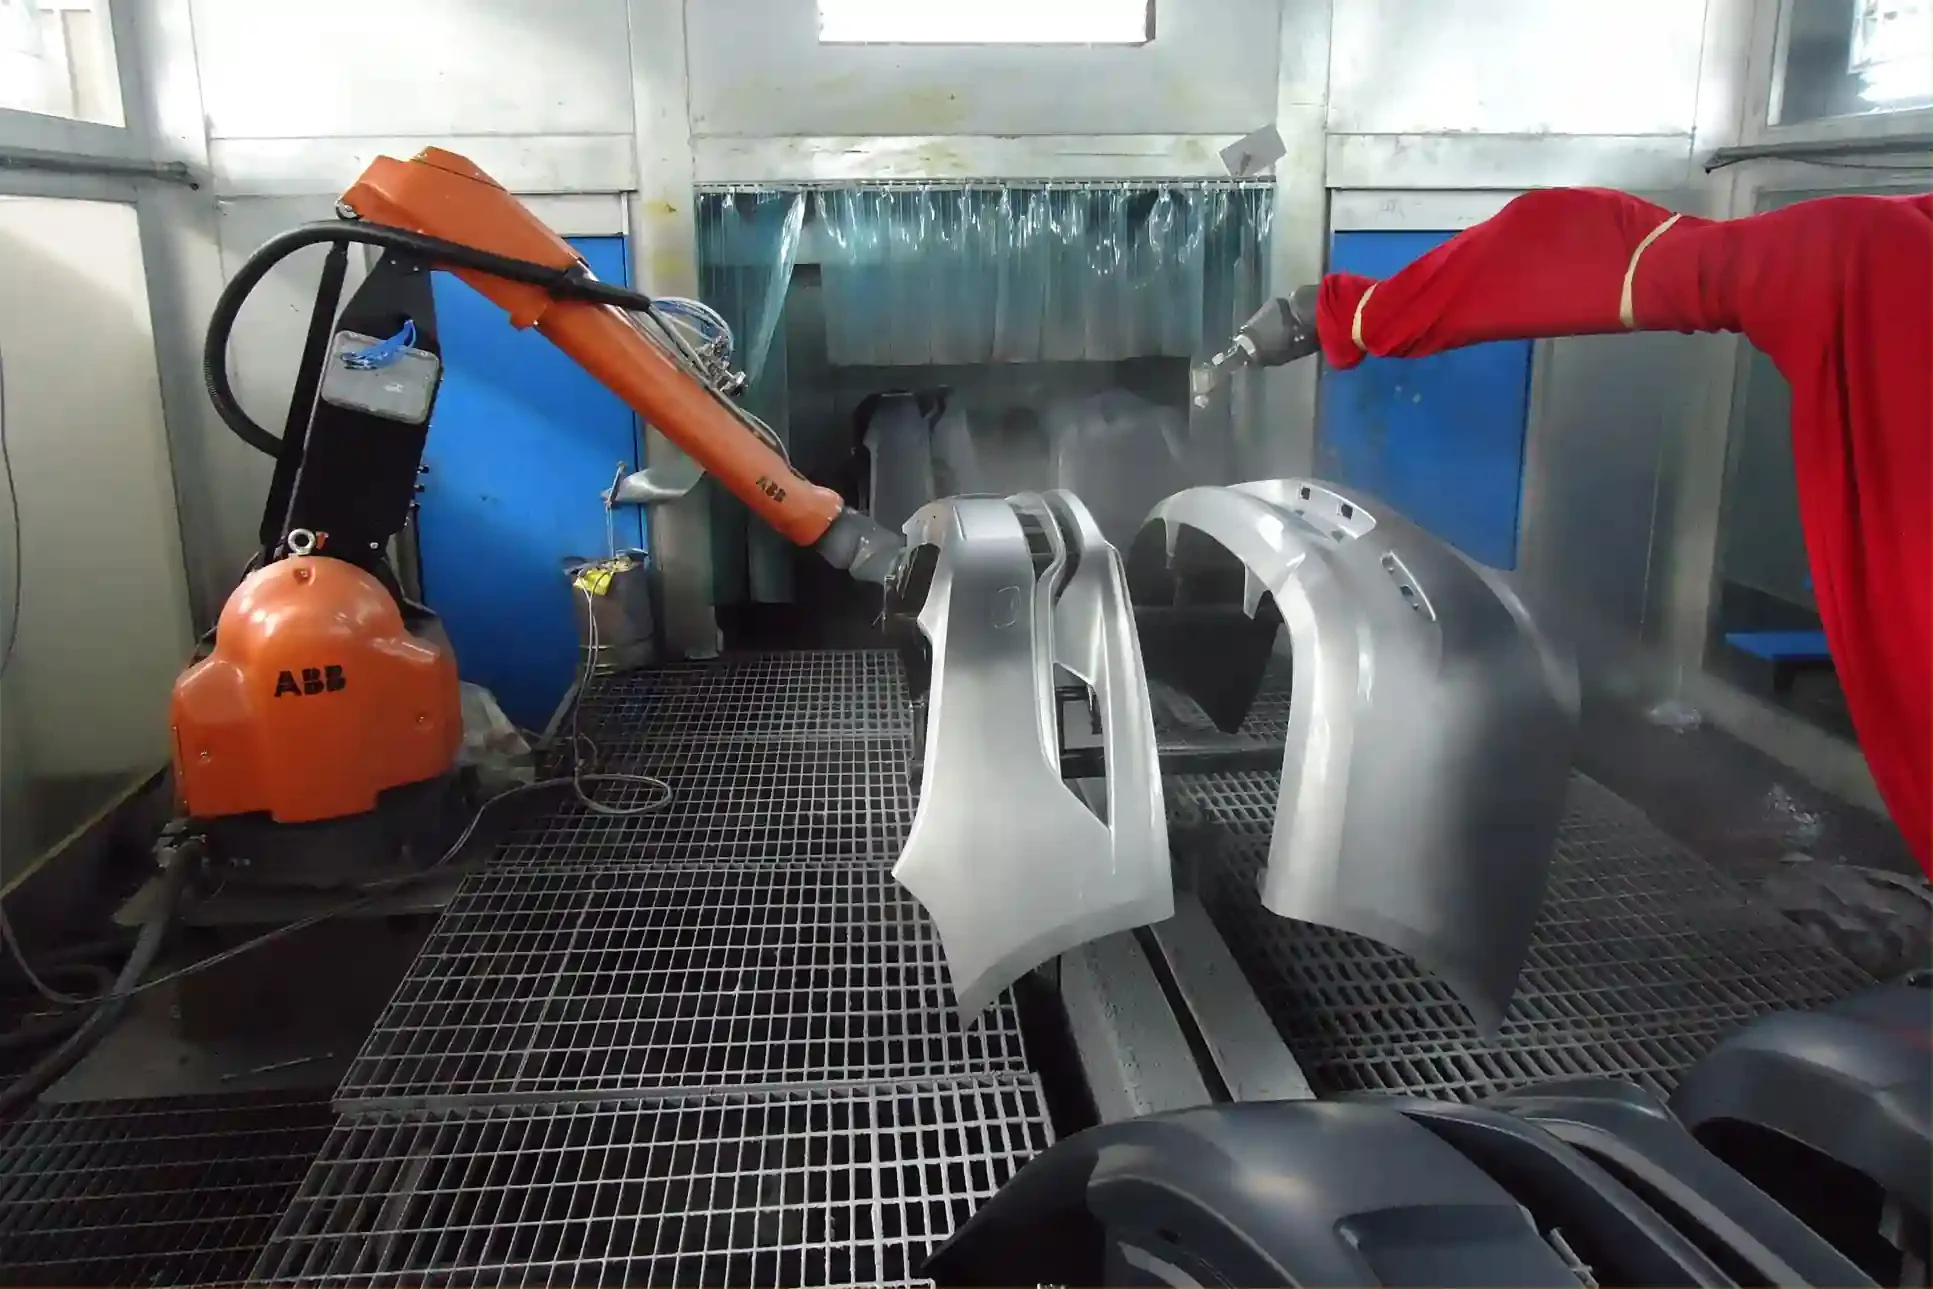
3C2B paint, matte paint, water transfer printing or chrome plating in our own lines.
Gloss, color, film thickness and adhesion are checked with our own instruments.
Finished surfaces are protected and packed for export.

L1 rotary automatic line with 24 stations and L2 overhead conveyor line, 3C2B paint system, UV clearcoat optional.
Spray booths ISO 8 (Class 100,000), flash-off and oven ISO 7 (Class 10,000).
Color ΔE*ab ≤1.0 (critical ≤0.8), total film 35–50 μm, cross-hatch adhesion grade 0–1.
28-tank automatic gantry line, Cu/Ni/Cr ≥32 μm, trivalent chrome as standard.
Appearance is checked in-house with a BYK micro-TRI-gloss meter, an X-Rite Ci64 spectrophotometer and a BYK coating thickness gauge, and parts can be cycled in our −40 to 150 °C temperature chamber. Durability tests are run by accredited outside labs (SGS, CTI, CNAS-accredited) to the methods in your specification:

The main ones are ABS, PC/ABS, ASA, PP and TPO. ABS and PC/ABS are used for rigid styling parts that are painted or plated, ASA for unpainted parts in the sun, and PP or TPO for bumpers and other impact parts.
Most bumper covers are talc-filled polypropylene or TPO, painted after an adhesion primer. Smaller aftermarket bumper parts such as lips and diffusers are often ABS or PC/ABS.
UV-stabilized ASA keeps its color and gloss in sunlight better than ABS. Weather-stable PP or TPO compounds are also used for textured flares and cladding.
No. We chrome plate plating-grade ABS (PA-727 / HR-500 equivalent). Ordinary PC/ABS, ASA and PP are not suitable for our plating line.
No. Property tables show typical published datasheet ranges from resin manufacturers. Your part’s grade and test values are confirmed in the quote and sample stage.
Yes, through partner composites factories. Our own factory makes molded plastic parts, including a carbon fiber look by water transfer printing or film.
We offer low MOQ on selected items. The quantity for your part is confirmed in your quote.
Send your drawing or sample and tell us how the part is used. We will recommend a material and finish and reply with a quote.